In an increasingly demanding industrial sector, the safety and reliability of sealing systems are essential to ensure the proper operation of plants and reduce the risk of downtime. For over 60 years, Fluiten has been designing and manufacturing high-performance mechanical seals, tailored to meet the specific needs of each production process.
Compliant with API 682 international standards, our double-pressurized sealing solutions with barrier fluid are ideal for applications involving toxic, flammable, H₂S-containing, or solid-laden liquids. In these critical environments, ensuring an effective isolation between the product and the external environment is crucial for operational safety and the integrity of the plant.
Advanced Barrier Fluid Management
To ensure optimal performance of double mechanical seals, Fluiten employs advanced barrier fluid management systems, including Plan 53B. This system, based on a pressurized and instrumented reservoir or a membrane accumulator pre-charged with air, maintains the desired pressure and ensures continuous protection of the seal.
Fluiten’s mechanical seals are designed with internal circulation devices, carefully engineered to provide an adequate fluid flow for heat dissipation generated by the friction of the seal itself. Critical parameters such as the PxV factor (pressure × velocity) and the heat transferred from the process are thoroughly analyzed to optimize performance and maximize the operating life of the sealing system.
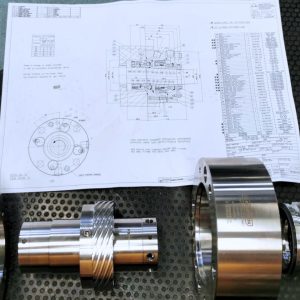
With a highly specialized technical team and over six decades of experience, Fluiten delivers tailor-made solutions for every industrial requirement. Our commitment to research and development enables us to offer increasingly efficient, safe, and reliable mechanical seals, helping to enhance plant performance and reduce maintenance costs.
Choosing Fluiten means partnering with a leader in mechanical sealing technology, dedicated to supporting companies with innovative solutions and high-level technical expertise.